Rotary Volumetric Filler – High‑Speed Fillers Accommodate a Wide Range of Containers and Products, from Water‑Thin to Heavy Syrups, Oils and Shampoos

July 24, 2025

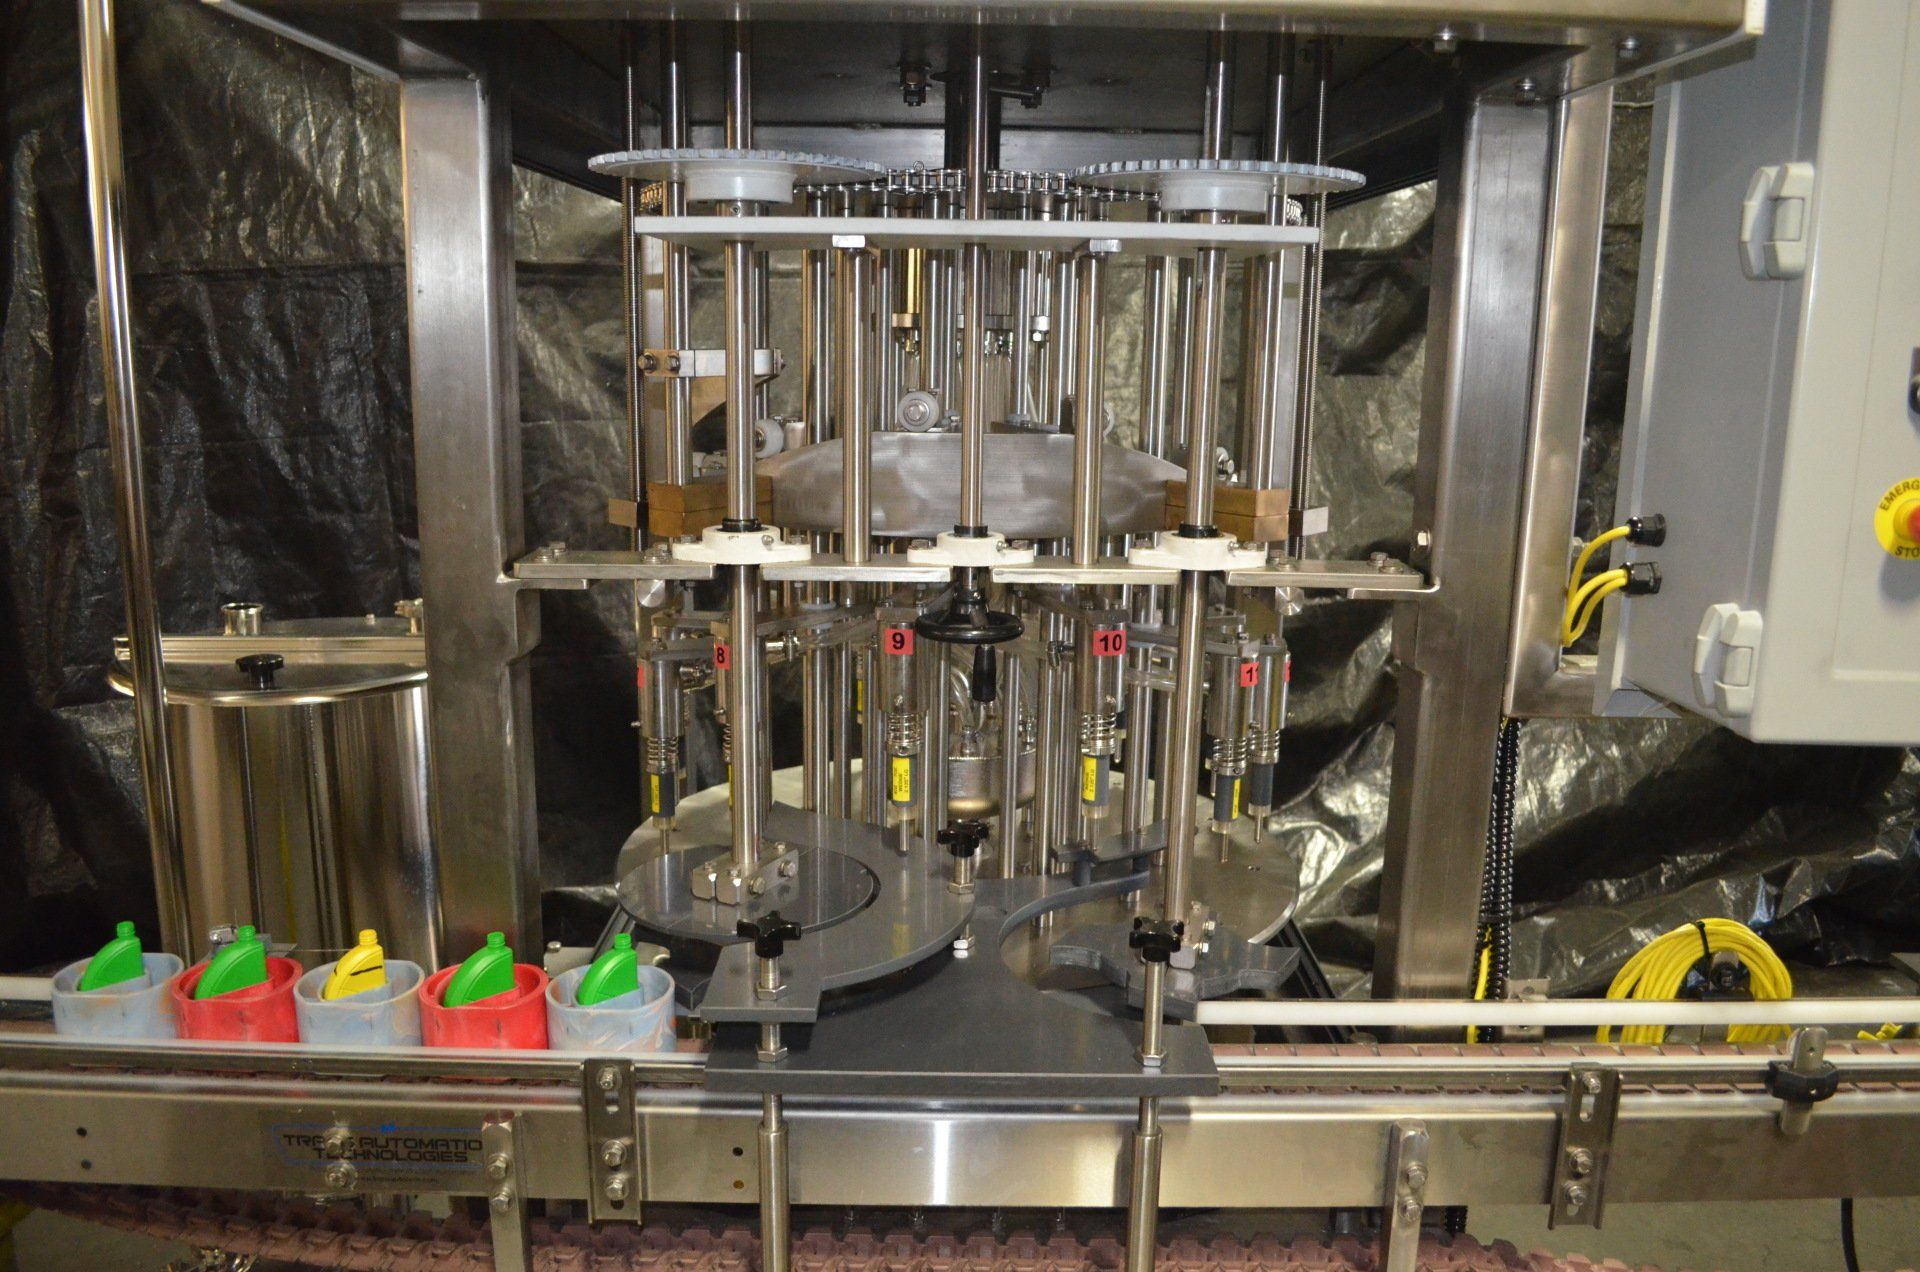
At Laub\Hunt, we understand that modern production lines demand high-speed volumetric filling coupled with industry-leading accuracy, versatility, and robust engineering. Our Rotary Volumetric Filler, also known as the Posifiller, delivers just that—precise, high-output filling for countless container and product types.

High Speed, High Throughput

Built for demanding operations, the Rotary Volumetric Filler runs at up to 600 containers per minute (cpm) while offering fill accuracy of ±¼ %, minimizing product waste and inconsistencies.
Its rotary design supports speeds up to 600 cpm and accommodates up to 120 nozzles on large-frame machines.


Wide Range Compatibility: From Thin to Thick

This filler is engineered to handle a broad viscosity range—from water-thin liquids like water or light juices, to heavier syrups, oils, detergents and shampoos. Its enclosed filling system ensures product integrity and precision across the spectrum. Containers from 1 oz to 5 gallon volumes are accommodated with minimal changeover time and tool-free adjustments.

Precision Mechanics at Work

At the heart of the Posifiller is a unique enclosed piston‑cylinder assembly. A free-floating piston delivers exact volumes by displacement between positive stops, controlled by an adjustable volume rod. The four‑way spool valve maintains balanced pressure and enables accurate two-phase pistoning for each fill.
These design features deliver consistent fill volumes and ensure extremely low deviation—critical in regulated or costly product environments.

Watertight Design for Hygiene and Efficiency

Sanitary operation is built into the design. No ambient air enters the system—from surge tank to nozzle—thanks to the closed construction of the Posifiller. This reduces contamination risk and maintains product quality.
The system is also
washdown-capable, with all drive motors placed atop the unit; and CIP (clean-in-place) product flush systems are standard or optionally automated.

Engineered for Flexibility and Ease

Designed for minimal downtime, the machine enables on‑the‑fly volume adjustment across stations via a motorized volume plate—ideal for format changes or multiple SKUs. Starwheels and nozzle assemblies allow tool‑free starwheel changes, making size changeovers fast and operator‑friendly.

Industry‑Grade Features

  • Stainless steel construction (T304 standard, optional T316 or specialty materials for caustic applications)
  • Individually adjustable cylinders and nozzles
  • Safety-interlocked guarding and AC drive with clutch
  • Premium options including explosion-proof (NEMA‑4X or NEMA‑7) electrics and automatic CIP
  • Conveyor lengths up to 10 ft with precision Delrin chain guides

Why Choose Laub\Hunt’s Rotary Volumetric Filler?

With unmatched precision, high-speed throughput, and broad product/container adaptability, Laub\Hunt’s Posifiller is trusted in food & beverage, personal care, chemicals, household products, and more. Whether filling shampoos, oils, syrups or beverages, this filler delivers speed, efficiency and flexibility you can rely on.
15 Quality Assurance Checks: Safety, Durability, and Final Sign-Off - Part 2
October 23, 2026
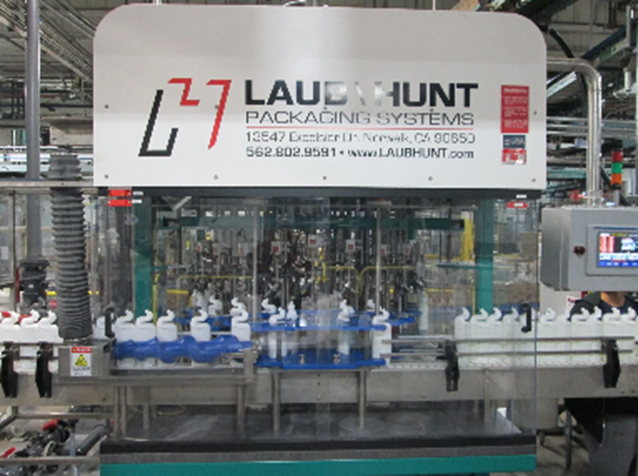
For bleach, detergents, and other foaming or chemically aggressive products, a dedicated suds test is performed to simulate actual operating conditions.
The 15 Quality Assurance Checks Every Machine Must Pass Before Shipment
October 18, 2026
Before any liquid filler leaves our facility, it must pass a structured series of 15 quality assurance checks that cover lubrication, mechanical alignment, leak integrity, safety, hygiene, and long‑run performance.
October 6, 2026
What Happens During Factory Acceptance Testing (FAT) Stages 5 - 7 Stage 5: Surface Finish, Coatings, and Safety Coatings and Finishes FAT also includes a review of protective coatings and surface finishes, important for both corrosion resistance and cleanability. Checks include: ● Confirming two coats of chlorinated rubber paint or equivalent on all iron surfaces where specified, especially for bleach and detergent applications. ● Ensuring no paint on any thread surfaces or leveling screws so adjustments remain possible. ● Verifying that brass wearing surfaces on sliders are not being scraped and are correctly aligned. These guidelines emphasize the importance of appropriate coatings and cleanable surfaces, particularly for food, beverage, and aggressive chemical products. Laub\Hunt’s attention to such details at FAT ensures long‑term durability and sanitation. Safety Devices and Nameplate As part of FAT, Laub\Hunt verifies: ● Presence and function of limit switches at the infeed star and on the infeed conveyor. ● Availability and accessibility of grease fittings and other routine‑maintenance points. ● Correct, legible nameplate data (model, serial, ratings), which customers will use for documentation and future parts orders. Best practices call for safety verification (guards, interlocks, e‑stops) and accurate identification plates as prerequisites for shipment. Laub\Hunt incorporates these checks to help customers meet safety and compliance requirements. Stage 6: Long‑Run Performance Trials Extended Run Test FAT is not limited to quick spot checks. Laub\Hunt performs extended run tests where the machine operates for a couple of hours at or near production speeds with water and bottles. During this period, technicians evaluate: ● What wears: observing cams, followers, sliders, and seals for abnormal heat, friction, or polish. ● What rubs or squeaks: diagnosing any contact or misalignment indicated by noise. ● Smooth transfer of bottles across bridge plates, transfer plates, donut plates, and conveyor chains, ensuring no stumbling or misfeeds. Longer‑duration FAT runs are essential for revealing latent issues that short trials miss—such as thermal growth, creeping misalignment, or intermittent jams. Laub\Hunt’s long‑run tests follow that logic and are documented as part of the FAT record. Torque Limiter and Overload Behavior Laub\Hunt’s checklist also calls for verifying the torque limiter: It must be adjustable so the machine can be pulled back while running and restarted from any position. During FAT, Laub\Hunt: ● Tests overload conditions to ensure the torque limiter slips or releases as designed. ● Confirms that the machine can resume operation without binding after an overload event. Tests of overload and emergency behavior ensures both equipment protection and operator safety. Including this in FAT means customers receive a machine whose protective systems have already been proven under controlled conditions. Stage 7: Special Tests for Detergent and Chemical Applications Suds and Chemical‑Behavior Tests For fillers intended for bleach, detergents, and other foaming or chemically aggressive products, Laub\Hunt performs specialized tests beyond standard water trials. These include: ● “Suds tests” using detergent or ammonia solutions to observe foam behavior in the bowl, valves, and overflow paths. ● Checks that level controls remain stable and that foam does not cause chronic false readings or spills. ● Validation that seals, coatings, and materials in contact with test solutions behave as designed. It is necessary to test performance under realistic process conditions, including foaming and temperature variations, before shipment. Laub\Hunt’s suds and chemical‑behavior tests are the result of decades’ experience in the bleach and household‑chemical markets. Stage 8: Spares, Accessories, and Documentation Counting Stars, Guides, and Spares A comprehensive FAT also ensures that everything promised in equipment order is present and accounted for. Laub\Hunt technicians: ● Count and record the number of stars and guides shipped. ● Verify the number of spare valves and confirm they are fully assembled and ready to use. ● Confirm that a grease gun and a tube of Parker O‑Lube (or equivalent) are packed with the filler. Best practices include checks that all auxiliary equipment, tools, and documentation are present, as these items are often critical to smooth commissioning. Final Documents and FAT Report Throughout the FAT, Laub\Hunt records: ● Test results, observations, and any deviations from expected performance. ● Adjustments made and final “zero settings” (e.g., fill volumes, speeds, and key alignment points). ● Outstanding minor items, if any, with a plan for resolution. Best practices call for a formal FAT report and acceptance certificate once criteria are met, with any minor punch‑list items documented separately. Laub\Hunt follows this model, ensuring that you have a shared, written record of what was tested and accepted before shipment. What FAT Means for You When Factory Acceptance Testing is complete, you receive a filler that has already: ● Been fully lubricated, aligned, and checked for mechanical integrity. ● Passed dry and wet functional checks, including leak tests, safety verifications, and extended runs. ● Demonstrated performance with your bottles under realistic conditions. ● Had its accessories, spares, and documentation verified and packed. Industry standards—and Laub\Hunt’s decades in liquid filling—show that this investment in the FAT dramatically reduces startup time, rework, and risk at your plant. By the time your machine reaches your dock, the heavy troubleshooting has already been done, allowing installation and commissioning to focus on integration and optimization rather than basic fixes. Contact us for more information. Also review stages 1-2 and stages 3-4.